
Polyresin & Polystone Statue Manufacturing in Vietnam
CT3D offers polyresin and polystone statue manufacturing in Vietnam for religious communities, brands, collectors, museums and interior projects. We work from a photo, a sketch, a 3D file or an existing statue, and deliver cast, assembled and hand-finished pieces – from a single commissioned figure to repeat batches cast from the same silicone molds.
Technical summary: CT3D’s polyresin and polystone statue manufacturing service in Vietnam follows a fully digital chain: 3D modeling or 3D scanning of the form, scaling in software, printing the master pattern in SLA/DLP resin or FDM, making multi-part RTV silicone molds, solid or hollow casting, then surface finishing with hand painting, airbrush, patina or cold-cast metal. This approach preserves anatomical proportions, enables consistent replication and lets us control statue weight right from the design stage.
Key Specifications
| Specification | Value |
|---|---|
| Master pattern | SLA/DLP resin (25–100 micron layers) or FDM (100–300 micron layers) |
| SLA tolerance | ±0.05–0.1 mm |
| Largest single resin print | Up to 800×800×500 mm; taller statues are printed in sections |
| Mold | Multi-part RTV silicone with a rigid mother mold |
| Casting | Solid casting or hollow rotational/slush casting |
| Materials | Polyresin, polystone, cold-cast bronze or brass |
| Delivery | Nationwide in Vietnam within 1–3 days after completion, workshop pick-up, or international shipping |

Polyresin Statue Manufacturing Capability
Statues are more demanding than typical gift items because they require three things at once: correct proportions, crisp surface detail (drapery folds, hair, facial features) and a structure that holds up to long-term display. Traditionally, artisans sculpt in clay and then build plaster molds; every size change means sculpting again. With a digital workflow, CT3D models the form once on the computer, outputs it in multiple sizes and edits the mesh directly without starting over. CT3D has more than 12 years of experience in 3D prototyping and has published projects such as the restoration of an Our Lady of La Vang statue, a large reclining Buddha statue, and a 1 m tall Catholic statue printed in SLA.
| Parameter | Value / option | What it means for statues |
|---|---|---|
| SLA layer height | 25–100 micron | Smooth faces, hands and drapery with minimal sanding |
| SLA tolerance | ±0.05–0.1 mm | Statue sections fit tightly with little filling |
| FDM layer height | 100–300 micron | Suited to large, low-cost master patterns |
| Large resin build volume | Up to 800×800×500 mm | Fewer sections for tall statues |
| Mold | RTV silicone + rigid mother mold | Captures undercuts |
| Casting method | Solid casting, hollow rotational/slush casting | Controls weight and prevents thermal cracking |
Source: 3D printing technology specifications in CT3D documentation.

How Polyresin Statues Are Made
- Scan or sculpt: an existing statue is 3D scanned, or our digital sculptors model the figure from photos and drawings. You approve multi-angle renders.
- Section and key: the model is split into head, body, arms and base along natural folds, with registration keys so the parts assemble precisely.
- Print the master: each section is printed in SLA resin for fine detail or FDM for large, lower-cost masters, then post-cured, sanded and primed.
- Make the mold: RTV silicone captures every undercut; a rigid mother mold holds the silicone in shape during casting.
- Cast: polyresin or polystone is poured solid, or rotated in the mold to build a hollow shell that saves weight and prevents thermal cracking.
- Assemble and finish: sections are joined, seams are filled, and the statue is painted, patinated or polished as cold-cast metal, then inspected.

Polyresin, Polystone and Cold-Cast: Choosing Material by Display Conditions
Polyresin is a thermoset plastic that cures with a catalyst at room temperature, so it can be poured into silicone molds without an oven. Adding stone powder produces polystone: heavier, with a stable base and the cool touch of stone. Coating the first layer in the mold with a resin and metal powder mix produces a cold-cast statue that can be polished to a bronze or brass sheen. Each variant brings different requirements for wall thickness, cure time and painting.
| Use conditions | Recommended material | Technical notes |
|---|---|---|
| Indoor display, altars, display cabinets | Painted polyresin | Moderately thin walls, light and easy to move |
| Statues needing a stable base and stone feel | Polystone | Increases weight; control shrinkage in thick sections |
| Metallic look on a limited budget | Cold-cast bronze/brass | Metal powder layer must be even so polishing does not expose the base |
| Semi-outdoor, under cover | Polyresin + UV-resistant topcoat | Thorough priming and protective coating; avoid standing water |
| Large outdoor pieces | Switch to composite FRP | See our composite FRP statue service |
Recommendations based on production experience, for reference only.

Digitization and Master Pattern Preparation (DfAM for Statues)
From photos, drawings or physical originals
If you have an existing statue to replicate or restore, CT3D 3D scans it to capture a point cloud, converts it to a triangle mesh, then repairs damaged areas and rebuilds chipped parts. If you only have photos or an idea, our digital sculptors model the form in sculpting software and send multi-angle preview renders so you can approve facial proportions, pose and clothing before printing. Learn more about statue restoration with 3D scanning and 3D printing on our 3D scanning service page.
Sectioning and mold parting
Tall statues are usually split into sections such as head, body, arms and base. Cut lines follow drapery folds or transitions in the form so joints are hard to see. Each section gets registration keys so it assembles in exactly the right position. Engineers also run a wall-thickness analysis and check overhangs, thin fingers and held objects to decide where to reinforce with metal core rods.
Finishing the master before molding
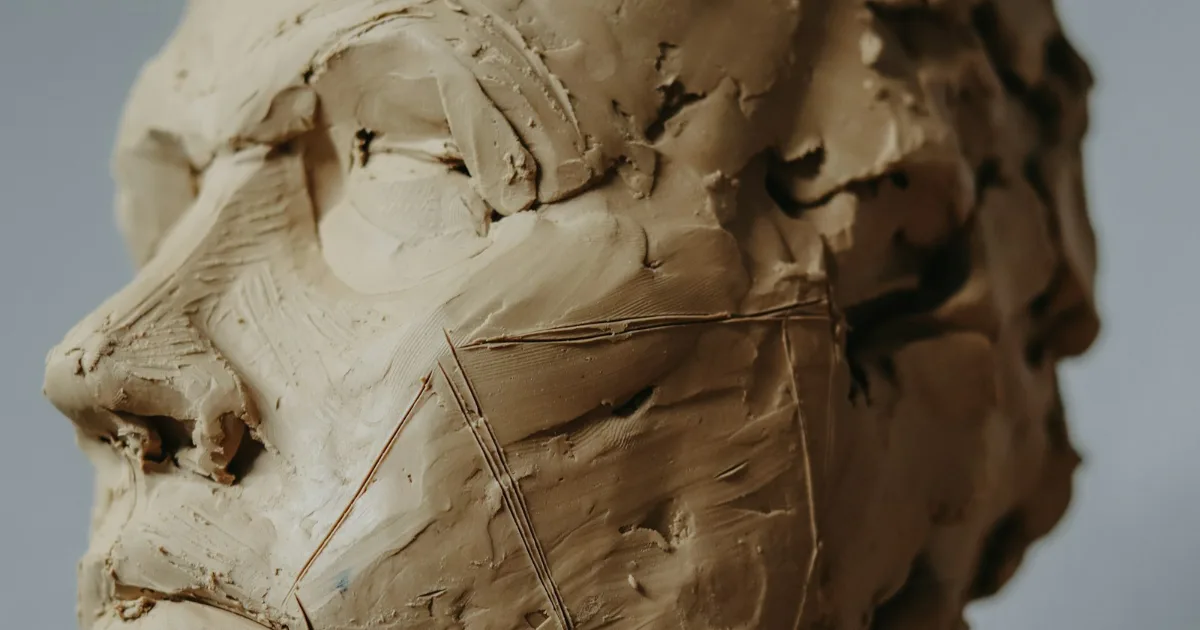
The printed master is washed, post-cured under UV, has its support structures removed, then is sanded, primed and sanded again. Every tiny mark on the master will repeat on every casting, so this stage is inspected under raking light. A detailed description of surface finishing is available in our guide to 3D print post-processing.
Design Guidelines for Cast Statues
Statues combine large volumes with very fine detail, so a few rules help them cast cleanly and survive transport. The figures below are typical industry starting points, not CT3D guarantees; we confirm the right values for your statue in the DFM review.
| Feature | Typical guidance | Reason |
|---|---|---|
| Hollow shell thickness | Typically a few millimeters, thicker at the base and joints | Saves weight and resin while keeping the statue rigid |
| Solid sections | Avoid large solid masses; hollow or core them | Thick resin heats up while curing and can crack |
| Fingers, staffs, held objects | Reinforce with metal core rods or thicken slightly | Thin protrusions are the first parts to break |
| Section cuts | Follow drapery folds, belts or changes in form | Joints are easier to hide after filling and painting |
| Registration keys | Model locating keys into each joint | Sections assemble in exactly the right position |
| Base | Wide, flat and slightly heavier than the top | Prevents tipping; polystone helps where stability matters |
| Fine relief detail | Keep detail deep enough to survive priming and paint | Very shallow texture can disappear under coatings |
Finishing Options for Statues
One mold can produce several finished versions of the same statue, which is useful when you sell or donate figures at different price points.
| Finish | Look | Typical use |
|---|---|---|
| Natural hand painting | Lifelike skin tones, robes and details | Devotional figures, characters, collectibles |
| Airbrush shading | Soft gradients and depth | Faces, drapery, larger surfaces |
| Patina | Aged stone or bronze appearance | Heritage replicas, garden and lobby statues |
| Faux bronze paint | Bronze look at paint cost | Budget metallic statues |
| Cold-cast bronze or brass | Real metal powder polished to a sheen | Premium statues and awards |
| Ivory white | Clean, single-tone finish | Religious and minimalist interiors |
| UV-resistant topcoat | Protective clear layer | Statues placed outdoors under cover |

Industry Applications
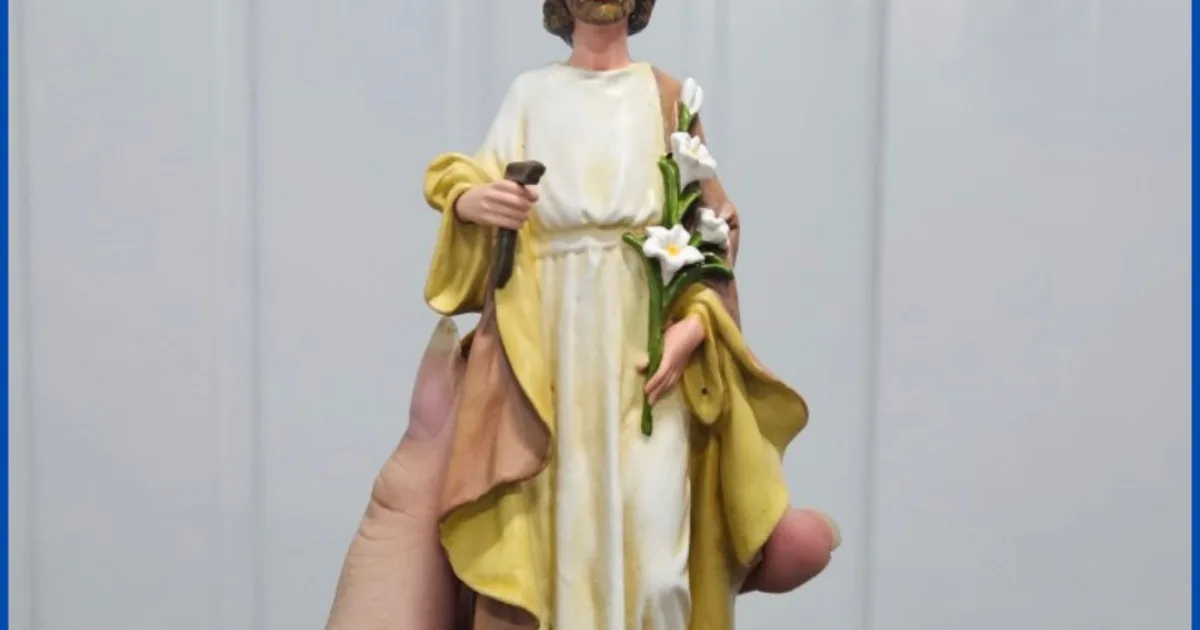
- Religious and devotional: Buddha statues, Catholic statues and small to mid-size devotional figures for churches, parishes, temples and retailers worldwide; see religious 3D printed statues.
- Brands and retail: desktop mascot characters, enlarged product models for display counters.
- Collectibles and entertainment: figures, limited-edition character statues, personalized statue bases.
- Museums and heritage sites: replicas of original statues for display while the originals are preserved.
- Architecture and interiors: reliefs, lobby statues, replicated ornamental details.
Polyresin vs Other Statue Processes
The right process depends on size, location, quantity and budget. This qualitative comparison reflects typical behavior of each route rather than measured data.
| Factor | Polyresin / polystone casting | Direct SLA 3D print | Composite FRP | Bronze casting |
|---|---|---|---|---|
| Typical size | Small to mid-size | Small to about 1 m, larger in sections | Large, several meters | Any, cost rises quickly with size |
| Best quantity | Repeat batches from one mold | One-offs and masters | One-offs or a few pieces | One-offs to small editions |
| Detail | Excellent | Excellent | Good, refined by hand | Excellent |
| Outdoor use | Under cover with UV topcoat | Indoor | Yes, with outdoor paint system | Yes |
| Relative cost | Low to medium per piece | Medium per piece | Medium to high | High |
For large outdoor pieces see our composite FRP statue service.
Quality Control for Cast Statues
CT3D inspects against these checkpoints: proportions compared with the approved file, fit of the joints, air bubbles on faces and hands, uniformity of the cold-cast layer, and paint color against the master sample. For hollow-cast statues, technicians check wall thickness by tapping and backlighting thin areas to prevent breakage during transport. For batch orders, the approved first article is kept as the reference standard for the whole batch.
| Defect | Cause | Countermeasure |
|---|---|---|
| Air bubbles on faces and fingers | Resin not flowing into small cavities | Brush a face coat first; vacuum degas when needed |
| Cracked statue base | Solid section too thick, exotherm | Hollow casting, insert a lightweight core |
| Misaligned joints | Missing registration keys | Add locating keys directly in the file |
| Blotchy cold-cast | Uneven metal powder distribution | Apply several even coats; inspect before pouring the core |
How to Order a Polyresin Statue
Send whatever you have – photos, a 3D file or the statue itself. Your files stay confidential and we sign an NDA on request; a free manufacturability (DFM) review is included with every quote.
- RFQ: send photos, STL/OBJ/STEP/3MF files or a physical sample via our Contact form; specify height, quantity, color and where the statue will be placed.
- DFM review: engineers propose the sectioning plan, wall thickness, solid or hollow casting, and the right material.
- Quotation: modeling, master pattern, mold and per-statue costs are itemized, with the delivery schedule.
- Digital approval and First Article Inspection (FAI): approve the 3D model, then approve the first painted statue.
- Production: casting, assembly, seam filling and finish painting to the approved sample.
- QC and delivery: visual inspection, crating with custom-fit padding; delivered nationwide within Vietnam in 1–3 days after completion, picked up at the workshop, or shipped internationally.
Why Choose CT3D for Polyresin Statues
- More than 12 years in 3D prototyping: published statue projects include an Our Lady of La Vang restoration, a large reclining Buddha and a 1 m Catholic statue printed in SLA.
- Digital accuracy: one 3D model can be output at several sizes without re-sculpting, and proportions are checked against the approved file.
- Weight control by design: sectioning, hollow casting and wall thickness are planned before the master is printed.
- Approval at every key stage: 3D model first, then a painted first article that becomes the standard for the batch.
- Clear communication: engineering support in English, itemized quotes and a fast reply to every request.
Frequently Asked Questions (FAQ)
Can polyresin statues be placed outdoors?
Yes, under cover and with a UV-resistant topcoat. For large statues fully exposed outdoors, CT3D recommends switching to composite FRP.
Can you enlarge a small statue I already have?
Yes. The statue is 3D scanned, the mesh is cleaned up and then scaled. Any soft details on the original are digitally re-sculpted before the master is printed.
How much heavier is polystone than polyresin?
It depends on the stone powder ratio and wall thickness. CT3D weighs the first article and reports the actual weight so you can plan shipping.
Can one statue be produced in different finishes?
Yes. The same mold can produce multiple versions: natural painted colors, faux bronze, ivory white or cold-cast.
How large can a polyresin statue be?
A single resin print can be up to 800×800×500 mm. Taller statues are split into sections with registration keys, printed, molded and cast separately, then assembled. For very large or fully outdoor statues we recommend composite FRP instead.
Can I approve the statue before it is cast?
Yes. You approve the 3D model from multi-angle renders first, then a fully painted first article. Series production only starts after both approvals.
Can you restore or replicate a damaged statue?
Yes. We 3D scan the original, repair damaged areas and rebuild chipped parts digitally, then print a new master. CT3D has published projects such as the restoration of an Our Lady of La Vang statue.
How are statues packed and shipped?
Each statue is crated with custom-fit padding. We deliver nationwide in Vietnam within 1–3 days after completion, offer pick-up at the workshop, and ship internationally on request.
Real Footage from the CT3D Workshop
Watch the video Making a 4-meter Buddha statue master with 3D printing and CNC produced by CT3D to get a clearer picture of our process and product quality. More videos are available on the Che Tao Vlog – CT3D channel.
Contact CT3D – Send Your Files for a Fast Quote
Whether you have a 3D file, a 2D drawing, photos or just an idea, you can send it to CT3D. Our engineers will review your files, advise on technology and materials, and send a quotation with a delivery schedule. Files can be sent online (STL, STEP, IGES, OBJ).
- Email: [email protected] – [email protected]
- Phone / Zalo: +84 975 008 728 (Mr. Thai) – +84 985 936 728 (Mr. Dang), or use our Contact form
- Head office: Binh Duong, Vietnam.
- Workshops: Ho Chi Minh City, Vietnam.
- Other workshops and drop-off points: Can Tho, Da Nang, Bien Hoa, Ba Ria – Vung Tau, Hanoi, Hai Duong, Hai Phong. Delivery nationwide and international shipping.
- Website: ct3dgroup.com – in3d.edu.vn
CT3D – 3D design & prototyping: 3D printing, 3D scanning, reverse engineering, silicone mold making, painting and finishing, CNC machining, composite fabrication, plus 3D printers and 3D printing materials.
Planning a polyresin or polystone statue?
Send photos, a 3D file or details of the original, with the height, quantity and finish you need. We reply quickly with a free DFM review and an itemized quote.